Aluminum vs Zinc Die Casting for Custom Hardware
Compare aluminum and zinc die casting using the part geometry, weight, finish, tooling, production volume and final functional requirements.
 Zaid ArshadManufacturing Content Author · KEC Tour

What to specify for this part
| Control point | Define in the RFQ | Risk if omitted |
|---|---|---|
| Mass | Density and part-size target | Material change alters product weight |
| Geometry | Wall, ribs, bosses and detail | The alloy/process combination cannot fill reliably |
| Environment | Temperature, corrosion and galvanic contacts | Finish alone is expected to solve compatibility |
| Finish | Cosmetic, protective and masking needs | Appearance varies by alloy and process |
Start with application constraints
Record load, temperature, weight limit, corrosion exposure, mating materials and appearance. Then shortlist specific alloy designations that meet those needs. Compare named aluminum and zinc casting alloys rather than broad material families alone. Zinc alloys are generally denser, so a geometry that looks economical may exceed the mass target. Confirm the required temperature and environmental performance from the selected alloy data.
Review geometry with the casting route
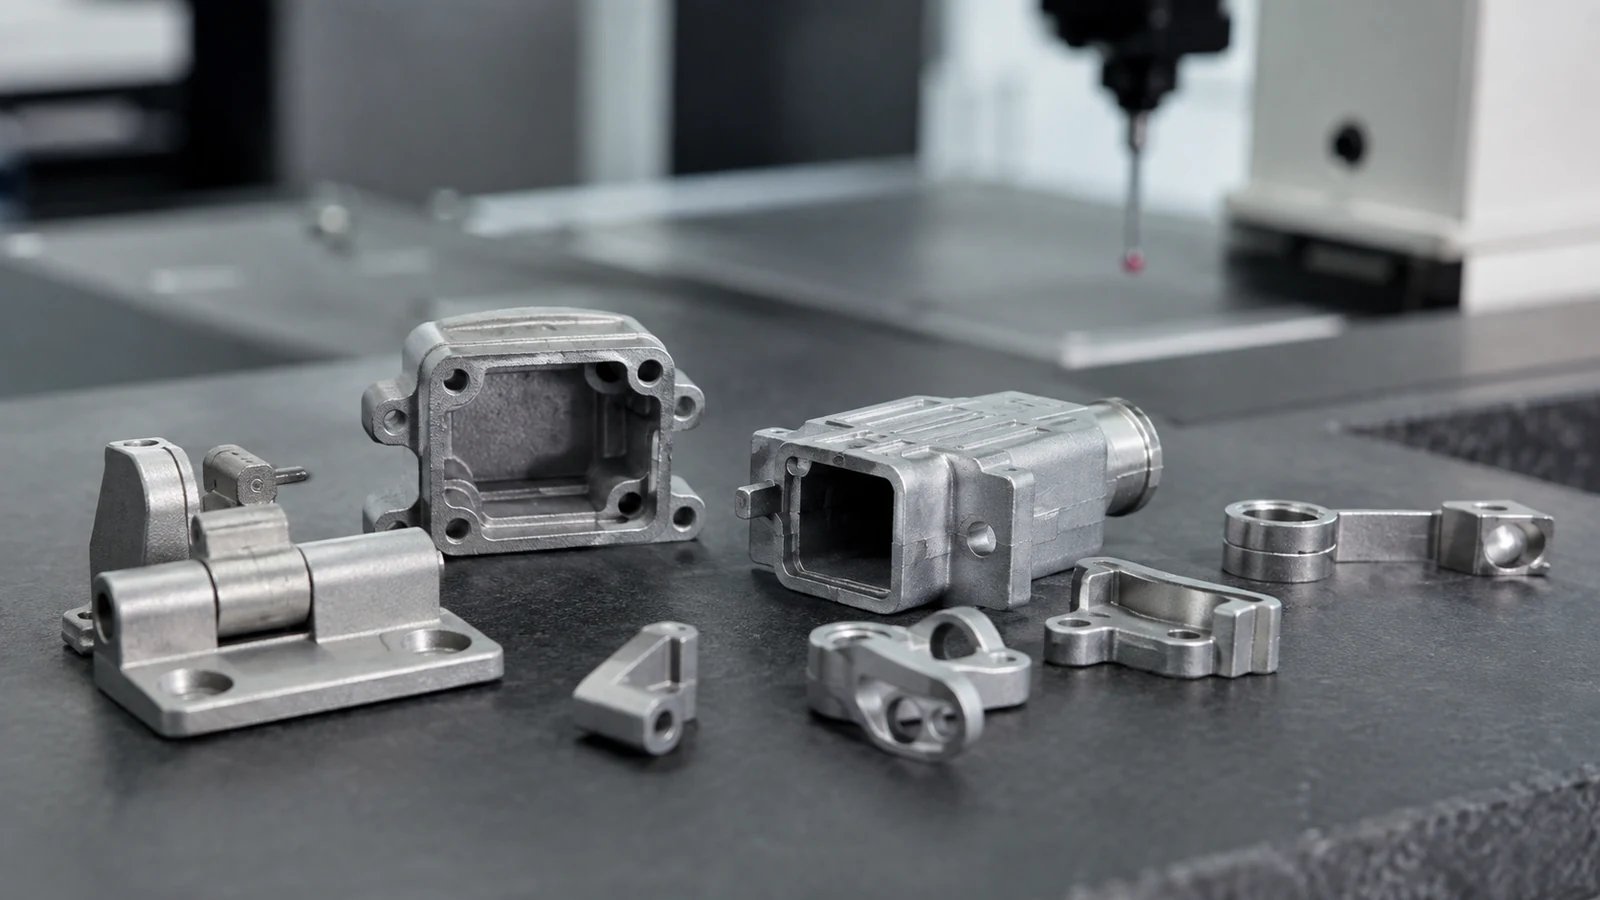
Wall transitions, draft, ejector locations, gates, overflows and parting line influence quality. A material cannot be chosen independently of the die and filling plan. Discuss the achievable detail, local wall transitions and the proposed die process with the caster. A thin rib that fills well in one alloy and process may need redesign in another. Approve gating, ejector marks and cosmetic boundaries before expensive tool details are fixed.
Account for secondary machining
Threaded holes, bearing seats, sealing faces and datum features may need machining. Compare tool wear, stock allowance, chip control and risk of exposing subsurface conditions. Identify the surfaces that need final machining for assembly. A precise cast-looking feature may still require drilling, tapping or boring to meet its functional limits. Include those operations and any inspection for exposed porosity in the cost comparison.
Approve finish on real samples
Color and texture depend on substrate, pretreatment, coating and viewing conditions. Use an approved boundary sample or documented range instead of adjectives such as “premium.” Review the complete coating and pretreatment system on the actual casting alloy. A polished appearance does not establish corrosion protection at an uncoated joint. Test the specified finish and mating conditions on representative samples before accepting a substitute alloy.
Frequently asked questions
Is zinc always stronger than aluminum?
Properties depend on the exact alloy, section, temperature and loading. Compare certified design data for the selected grades.
Which is better for thin walls?
The answer depends on geometry, size, process and supplier capability; request a casting DFM review.
Can aluminum and zinc use the same coating?
Finishing routes and pretreatments differ. Specify performance and confirm the process for the selected alloy.
Should I permit material substitution?
Only through a documented approval that covers mechanical, environmental, finishing and compliance requirements.
Sources and further reading
Send KEC Tour the relevant drawing and interface requirements for review of the proposed manufacturing route.
Zaid Arshad
Manufacturing Content Author · KEC TourZaid Arshad writes practical manufacturing guides for engineers and sourcing teams evaluating custom fittings, CNC-turned parts, sheet-metal components, stampings and die-cast parts. His articles focus on clearer RFQs, supplier evidence, inspection planning and drawing-to-production decisions.
View author profileRelated engineering guides

Engineering Changes for Custom Metal Assemblies: Control the Cutover
Link revised drawings, purchased parts, work in progress and inspection so a design change reaches the correct production units.
Read article
Burr Direction on Stamped Parts: Put the Functional Edge on the Drawing
Specify the acceptable edge condition and orientation where stamped parts contact seals, wires, hands or mating surfaces.
Read article
How to choose stainless steel grades for non-standard fittings
A practical guide for balancing corrosion resistance, machining stability, pressure use, surface finish, and cost.
Read articleTurn your requirements into a production-ready RFQ.
Share your CAD file, material, critical dimensions, finish and target volume. KEC Tour will review the process route before quoting.