Bend Allowance and K-Factor for Custom Sheet Metal Parts
Use material, bend radius, tooling and validated allowance to connect a sheet metal flat pattern with the required formed dimensions.
 Zaid ArshadManufacturing Content Author · KEC Tour

What to specify for this part
| Control point | Define in the RFQ | Risk if omitted |
|---|---|---|
| Thickness | Actual stock range, not only nominal gauge | Flat length shifts |
| Inside radius | Drawing requirement versus produced radius | Model and tool result diverge |
| Tooling | Punch, V-opening and bending method | Neutral-axis assumption changes |
| Control | Formed dimensions or buyer-supplied flat | Two parties control conflicting outputs |
Understand what the value does
Bend allowance estimates arc length along the neutral axis; bend deduction relates outside dimensions to the flat. K-factor locates the neutral axis as a fraction of material thickness for the selected calculation. For a bend angle in radians, a common allowance expression is angle multiplied by the sum of inside radius and K times thickness. The K value is a process assumption, not a universal property of the alloy. Confirm which angle convention the CAD system uses before comparing two calculations.
Use supplier-specific evidence
A handbook value can start a prototype, but repeat production should use bend coupons or validated bend tables for the actual material and tools. Record grain direction and measured radius with the result. Use coupons from the intended material thickness and record the punch, die opening and produced radius. Measure the formed result and adjust the bend table from that evidence. Repeat the check after a material or tooling change that could alter springback.
Choose the controlling definition
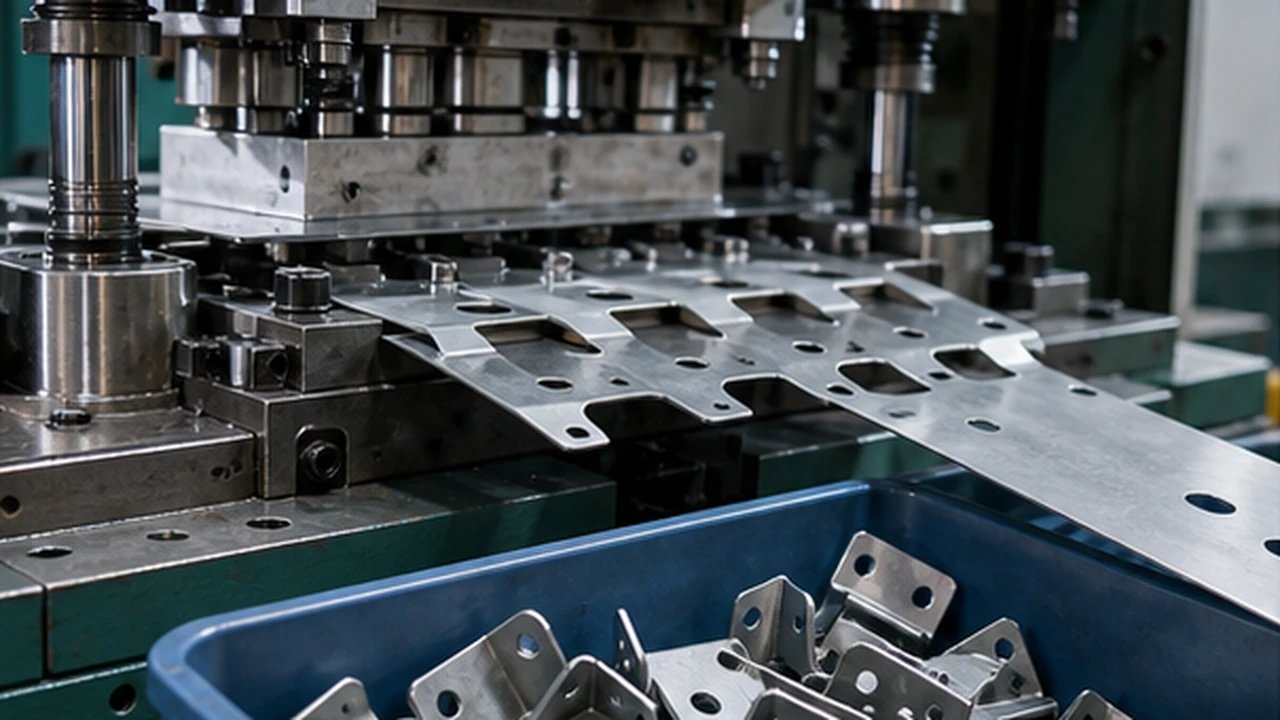
If the formed assembly is what matters, control formed dimensions and allow the fabricator to develop the flat. If the buyer supplies a released flat, agree who owns correction after trial bends. State the controlling datums and final flange relationships on the formed drawing. An unexplained flat-pattern correction can make future revisions difficult to reproduce. Retain the validated bend parameters with the manufacturing revision and clarify who maintains them.
Validate multi-bend stacks
Small error at one bend can accumulate across an enclosure or bracket. First-article inspection should measure the functional datum structure, not only individual flange lengths. A small angular error becomes a larger position error at the end of a long flange. Inspect the assembled mounting planes and hole locations, not only a list of bend angles. Use a representative enclosure or fixture to reveal a cumulative mismatch before the full batch is cut.
Frequently asked questions
Is K-factor fixed for stainless steel?
No. It changes with the bend process, radius-to-thickness ratio, tooling, material condition and other variables.
What is the bend-allowance formula?
A common form uses bend angle multiplied by the radius plus K times thickness; confirm conventions and units with the fabricator.
Should the drawing include K-factor?
Only when the buyer intentionally controls flat-pattern development. Otherwise provide formed geometry and let validated shop data drive the flat.
How do I improve first-article accuracy?
Share material/thickness, grain, inside radius and critical formed dimensions, then approve a trial result before volume.
Sources and further reading
Send KEC Tour the relevant drawing and interface requirements for review of the proposed manufacturing route.
Zaid Arshad
Manufacturing Content Author · KEC TourZaid Arshad writes practical manufacturing guides for engineers and sourcing teams evaluating custom fittings, CNC-turned parts, sheet-metal components, stampings and die-cast parts. His articles focus on clearer RFQs, supplier evidence, inspection planning and drawing-to-production decisions.
View author profileRelated engineering guides

Engineering Changes for Custom Metal Assemblies: Control the Cutover
Link revised drawings, purchased parts, work in progress and inspection so a design change reaches the correct production units.
Read article
Burr Direction on Stamped Parts: Put the Functional Edge on the Drawing
Specify the acceptable edge condition and orientation where stamped parts contact seals, wires, hands or mating surfaces.
Read article
How to choose stainless steel grades for non-standard fittings
A practical guide for balancing corrosion resistance, machining stability, pressure use, surface finish, and cost.
Read articleTurn your requirements into a production-ready RFQ.
Share your CAD file, material, critical dimensions, finish and target volume. KEC Tour will review the process route before quoting.