Custom Stainless-Steel Adapters: Material, Threads, Finish and Inspection
Specify stainless adapters with clear requirements for alloy, thread system, sealing interface, finish, cleanliness and verification.
 Zaid ArshadManufacturing Content Author · KEC Tour

What to specify for this part
| Control point | Define in the RFQ | Risk if omitted |
|---|---|---|
| End A / End B | Complete interface callout for each end | One side is assumed from a sample |
| Orientation | Clocking between flats, ports or elbows | Assembly points in the wrong direction |
| Material | Exact grade and permitted substitutions | Corrosion or certification mismatch |
| Traceability | Part/revision marking and lot records | Repeat orders cannot be reconciled |
Treat each end as its own specification
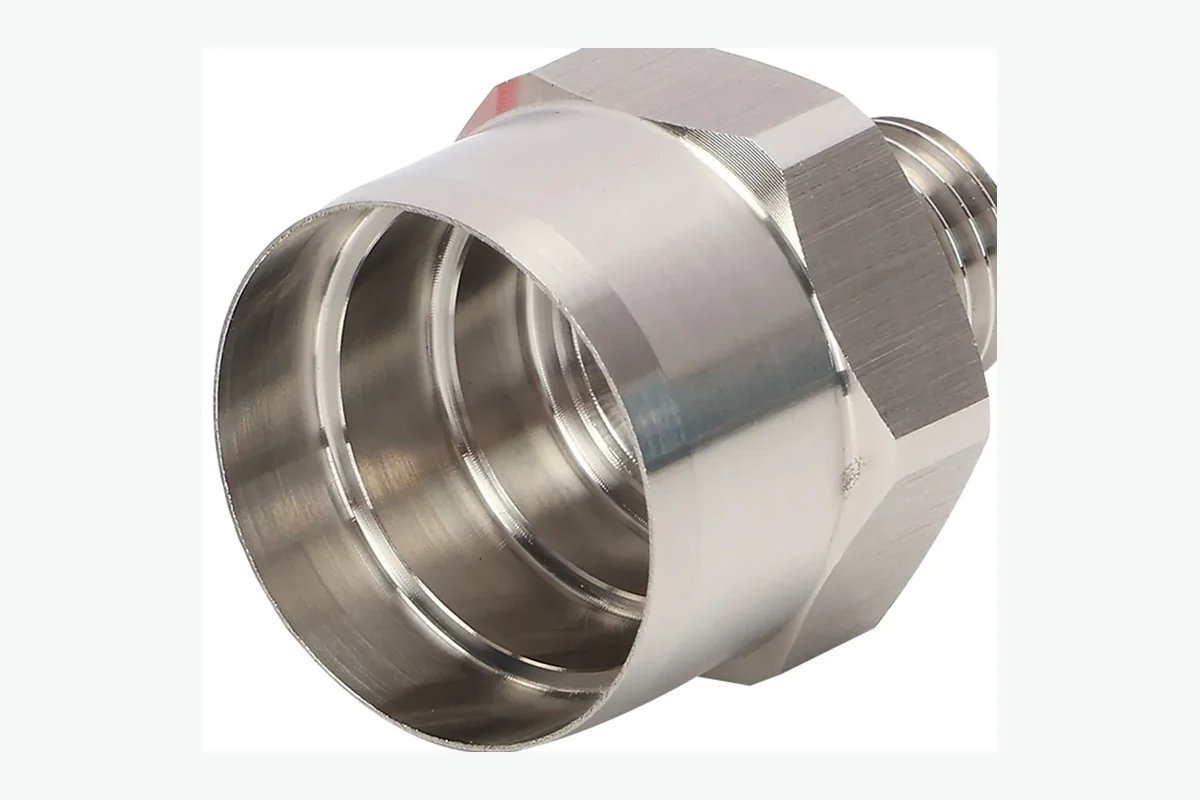
List thread standard, size, class, depth, gauge and sealing feature for both connections. For mixed standards, add a section view so no one infers the transition from the title. A reducing adapter can have a tapered thread at one end and a parallel face-sealed interface at the other. Name both standards and show where each seal is formed. Keep the gauge and inspection requirements separate so the easier end does not become the only acceptance check.
Decide how the part will be held and tightened
Wrench flats, hex size, tool clearance and installation envelope affect machining and field use. If orientation matters at torque, state the acceptable angular window and test method. Check that a wrench can engage the flats after adjacent hardware is fitted. Avoid relying on thread tightening alone to achieve a precise clocking angle unless the interface is designed for that purpose. Include the assembly envelope in the drawing review before adding an unnecessary secondary milling setup.
Select the finish around function
Passivation can support stainless cleanliness and corrosion performance; electropolishing also changes surface topography. Specify a standard and acceptance test when required instead of requesting an undefined “medical finish.” For a sealing land, determine whether material removal during polishing changes its geometry. Passivation and electropolishing serve different purposes and should not be substituted without approval. Define final thread and surface acceptance after the complete process route.
Approve a repeatable control plan
For recurring orders, record material heat/lot identification, gauge status, first-article results, finish batch and packaging method. A golden sample alone is not a complete specification. Retain the interface drawing and the measured first article as complementary records. If an approved material equivalent is used, identify the affected order and heat rather than changing the general specification silently. Review gauge suitability whenever the thread standard or finish changes.
Frequently asked questions
Can I quote from an existing adapter sample?
Yes for feasibility, but production should use a measured and approved drawing with confirmed thread and material requirements.
Should the supplier choose 304 or 316?
Provide the grade or a documented substitution process. The application owner must decide corrosion and compliance needs.
How is clocking inspected?
Define reference features, tightening condition and angular acceptance on the drawing or inspection instruction.
What finish should I request?
Name the process, applicable standard, cosmetic boundary and any verification such as free-iron or corrosion testing.
Sources and further reading
Send KEC Tour the relevant drawing and interface requirements for review of the proposed manufacturing route.
Zaid Arshad
Manufacturing Content Author · KEC TourZaid Arshad writes practical manufacturing guides for engineers and sourcing teams evaluating custom fittings, CNC-turned parts, sheet-metal components, stampings and die-cast parts. His articles focus on clearer RFQs, supplier evidence, inspection planning and drawing-to-production decisions.
View author profileRelated engineering guides

Engineering Changes for Custom Metal Assemblies: Control the Cutover
Link revised drawings, purchased parts, work in progress and inspection so a design change reaches the correct production units.
Read article
Burr Direction on Stamped Parts: Put the Functional Edge on the Drawing
Specify the acceptable edge condition and orientation where stamped parts contact seals, wires, hands or mating surfaces.
Read article
How to choose stainless steel grades for non-standard fittings
A practical guide for balancing corrosion resistance, machining stability, pressure use, surface finish, and cost.
Read articleTurn your requirements into a production-ready RFQ.
Share your CAD file, material, critical dimensions, finish and target volume. KEC Tour will review the process route before quoting.