What Drives CNC Turning Cost for Stainless Connectors?
Understand how stainless grade, stock, geometry, threads, tooling, deburring and inspection affect the cost of a custom CNC-turned connector.
 Zaid ArshadManufacturing Content Author · KEC Tour

What to specify for this part
| Control point | Define in the RFQ | Risk if omitted |
|---|---|---|
| Stock | Bar diameter, grade, availability and yield | Large removal volume and scrap |
| Cycle | Tool paths, drilling depth, threading and deburring | Small details dominate spindle time |
| Setup | Number of orientations and special workholding | Low quantities carry setup heavily |
| Quality | Tolerance, finish, gauging and documentation | Inspection can rival cutting time |
Separate recurring from one-time cost
Ask the quote to show programming, fixtures, gauges or samples separately from unit machining. This makes prototype and production prices comparable. For an illustrative order, a $300 setup and a $12 recurring cost produce a $72 unit price at five pieces and $18 at fifty pieces. These are arithmetic examples rather than KEC Tour prices. Changing inspection or stock assumptions between quantities would invalidate the comparison.
Find the cycle-time features
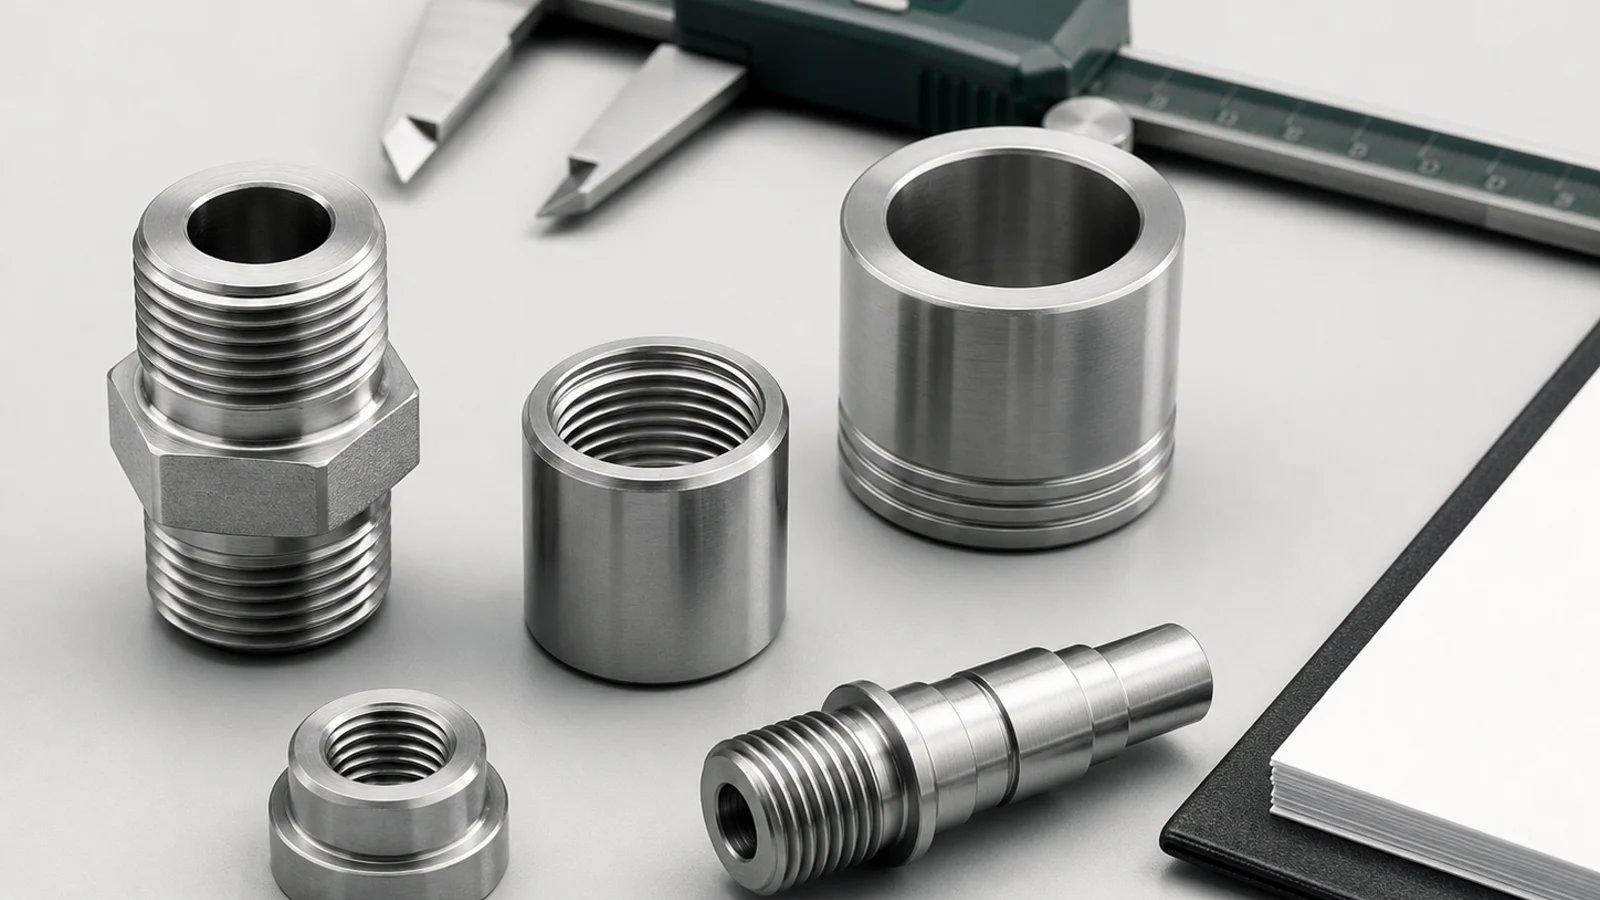
Deep small holes, long threads, thin walls, sharp internal corners and repeated tool changes slow production. A DFM review should identify the feature and the specific alternative, not just say “tolerance too tight.” A deep axial hole can take longer than the visible outside turning. Ask for alternatives such as a shorter passage or permitted drill-point clearance where function allows. Price the revised route against the original so the proposed saving has a traceable cause.
Use volume honestly
Price breaks only make sense when the supplier can run a stable batch and buy material efficiently. Forecast ranges and call-off expectations are more useful than an inflated annual number. A forecast of 10,000 parts does not create that purchasing volume if releases arrive as ten pieces at a time. State minimum release quantities and the period over which demand is expected. Confirm who carries inventory and when material or fixture commitments become payable.
Evaluate total usable-part cost
Include first-article approval, finish fallout, freight, packaging and defect response. A lower quoted part price can be more expensive if it creates assembly sorting or line stops. Compare cost per accepted usable part on a consistent scope. An inexpensive connector that requires incoming sorting may cost more in inspection labor than it saves in cutting. Track the specific failure mechanism and prevention cost instead of adding an unexplained risk percentage.
Frequently asked questions
Why is the prototype price high?
Programming, setup, material minimums and inspection are divided across few parts.
Does a looser tolerance always reduce price?
Only if it removes a real process or inspection constraint. Ask the supplier which requirement changes the route.
Can changing material lower cost?
Possibly, but substitutions must be approved against corrosion, strength, joining and compliance needs.
How can buyers compare quotes?
Normalize quantity, material, finish, inspection, packaging, Incoterm, tooling ownership and lead-time start point.
Sources and further reading
Send KEC Tour the relevant drawing and interface requirements for review of the proposed manufacturing route.
Zaid Arshad
Manufacturing Content Author · KEC TourZaid Arshad writes practical manufacturing guides for engineers and sourcing teams evaluating custom fittings, CNC-turned parts, sheet-metal components, stampings and die-cast parts. His articles focus on clearer RFQs, supplier evidence, inspection planning and drawing-to-production decisions.
View author profileRelated engineering guides

Engineering Changes for Custom Metal Assemblies: Control the Cutover
Link revised drawings, purchased parts, work in progress and inspection so a design change reaches the correct production units.
Read article
Burr Direction on Stamped Parts: Put the Functional Edge on the Drawing
Specify the acceptable edge condition and orientation where stamped parts contact seals, wires, hands or mating surfaces.
Read article
How to choose stainless steel grades for non-standard fittings
A practical guide for balancing corrosion resistance, machining stability, pressure use, surface finish, and cost.
Read articleTurn your requirements into a production-ready RFQ.
Share your CAD file, material, critical dimensions, finish and target volume. KEC Tour will review the process route before quoting.